المنتجات المميزة

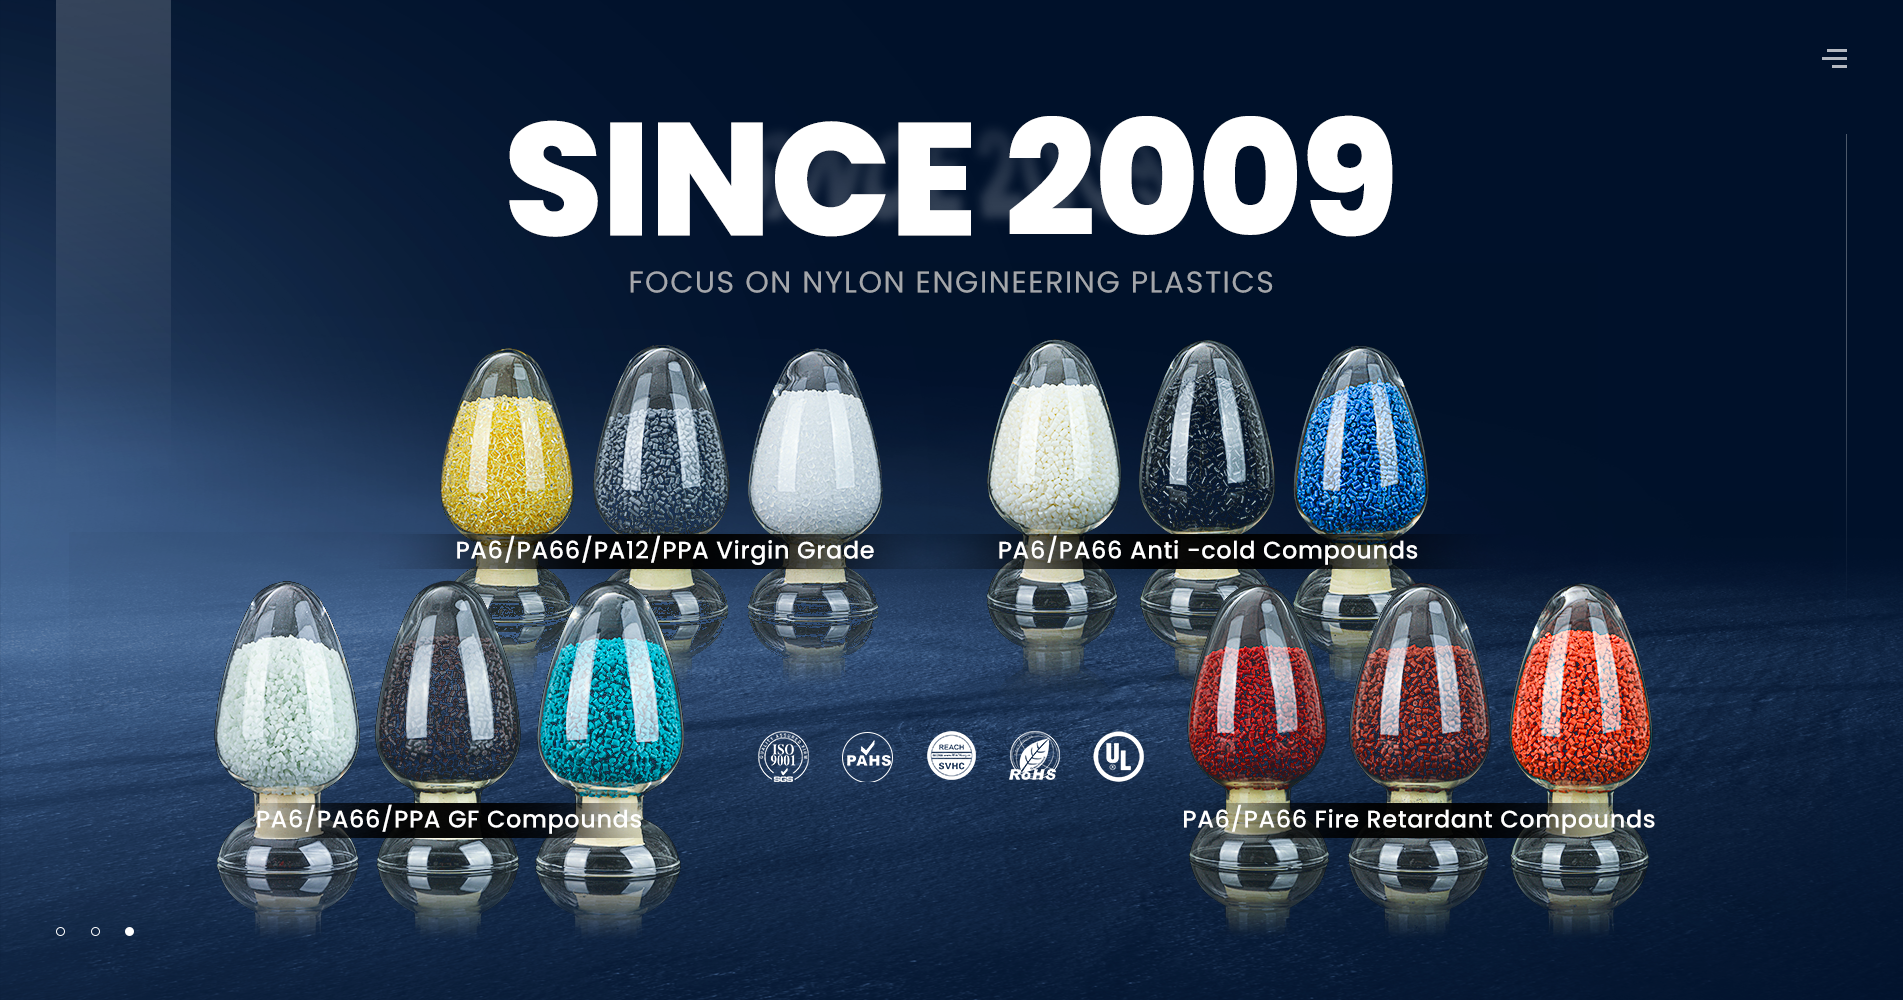
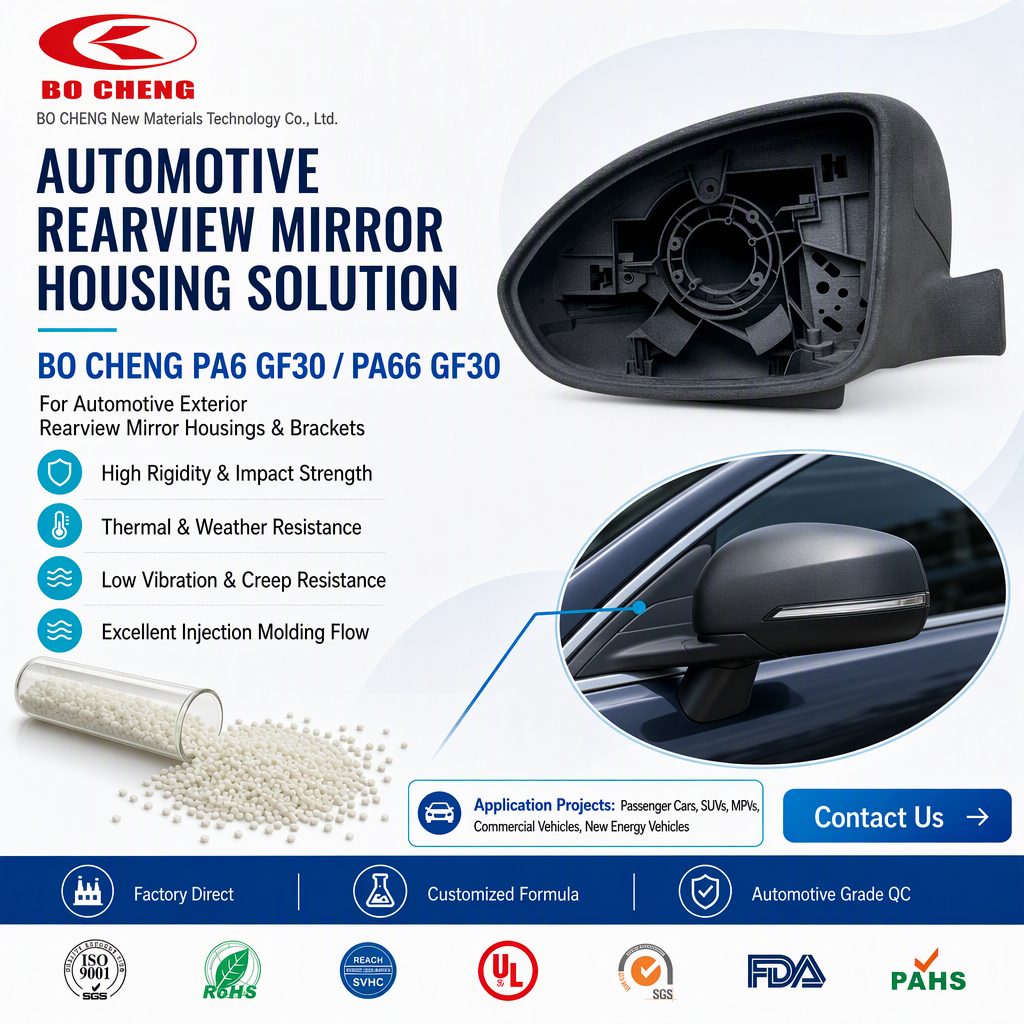
نحن نركز على إنتاج وتطوير وتطبيق النايلون PA6، وتعزيز PA66، والتصلب، والتوصيل الحراري، ومقاومة الحرارة، ومقاومة اللهب وغيرها من البلاستيك المعدل الخاص.
  • PA66 Resin
    PA66 EPR27 نايلون 66 معدل عالي التأثير من الدرجة البكر

    نايلون PA66 عالي الجودة من الدرجة العذراء: راتينج بولي أميد 66 (PA66) عالي الجودة وغير معدل بتركيبة EPR27، مما يضمن الاتساق والأداء المتفوق. التطبيقات الرئيسية: مثالي لأجزاء السيارات والأجهزة الإلكترونية والأدوات الكهربائية والتروس الصناعية. توريد المصنع مباشرة: تتوفر خيارات قابلة للتخصيص لتلبية متطلبات المعالجة والأداء المحددة.

  • Molding Process Glass Fiber Reinforced Material
    مادة ألياف زجاجية عالية القوة PA6 GF30 طبيعية/سوداء

    مادة PA6 GF30 من الدرجة المصبوبة بالحقن، معززة بألياف زجاجية بنسبة 30% لتعزيز القوة والصلابة ومقاومة الصدمات.متوفر باللونين الطبيعي والأسود، ومناسب للتطبيقات الصناعية المتنوعة.مثالي لأجزاء السيارات والأجهزة الإلكترونية والأدوات الكهربائية والمعدات الصناعية، مما يضمن أداءً ثابتًا في ظل ظروف الضغط العالي.توريد مباشر من المصنع مع تركيبات قابلة للتخصيص لتلبية احتياجات التطبيقات المختلفة.

  • Engineering Plastic for High Performance
    مادة PA66 GF30 المقواة بألياف زجاجية لتعزيز القوة والمتانة

    مادة PA66 GF30 من الدرجة المصبوبة بالحقن، معززة بألياف زجاجية بنسبة 30% لتحسين قوة الشد والصلابة ومقاومة الصدمات.مثالي لأجزاء السيارات والأجهزة الإلكترونية والأدوات الكهربائية والمعدات الصناعية، مما يضمن أداءً متفوقًا في البيئات الصعبة.توريد مباشر من المصنع مع خيارات قابلة للتخصيص لتلبية متطلبات التطبيقات المتنوعة.

  • 30% Glass Fiber Reinforced PA6
    مادة PA6 GF30 FR V0 عالية القوة مقاومة للحريق معززة بألياف زجاجية

    مادة PA6 GF30 FR V0 من فئة الحقن، معززة بألياف زجاجية بنسبة 30% لتحقيق قوة وصلابة فائقة.مادة مقاومة للهب حاصلة على شهادة UL94 V-0، مما يوفر مقاومة ممتازة للحريق للتطبيقات الحرجة للسلامة.مثالي لأجزاء السيارات والأجهزة الإلكترونية والمعدات الصناعية، مما يضمن أداءً موثوقًا به في درجات الحرارة العالية.توريد مباشر من المصنع مع تركيبات قابلة للتخصيص لتلبية متطلبات التطبيق المتنوعة.

  • PA66 GF30 FR V0 Supplier
    مادة PA66 GF30 FR V0 المقواة بألياف زجاجية مقاومة للهب

    مادة PA66 GF30 FR V0 من فئة القولبة بالحقن، معززة بألياف زجاجية بنسبة 30% لتعزيز القوة والصلابة. مثبط للهب بتصنيف UL94 V-0، ضمان أعلى مستوى من السلامة من الحرائق في التطبيقات الحرجة. مثالي لمكونات السيارات والأجهزة الإلكترونية والمعدات الصناعية، مما يوفر أداءً موثوقًا به في ظل الظروف القاسية. توريد مباشر من المصنع مع تركيبات قابلة للتخصيص لتلبية متطلبات الصناعة المختلفة.

  • Cold Weather Flexibility
    مادة PA6 المضادة للبرد متينة ومقاومة للبرد

    مادة PA6 من الدرجة الحقنية، مصممة لمقاومة البرد الفائقة والمتانة في البيئات ذات درجات الحرارة المنخفضة.مثالي لأجزاء السيارات والمعدات الخارجية والتطبيقات الصناعية التي تتطلب أداءً موثوقًا به في البرد القارس.توريد مباشر من المصنع مع تركيبات قابلة للتخصيص لتلبية احتياجات التطبيق المحددة.

  • Industrial Tools for Extreme Climates
    مادة PA66 المقاومة للبرد ومقاومة الصدمات العالية

    نايلون PA66 عالي الأداء ومقاوم للبرد: تمت صياغته خصيصًا للحفاظ على المرونة ومقاومة الصدمات والسلامة الهيكلية في البيئات ذات درجات الحرارة المنخفضة. التطبيقات الرئيسية: مثالي لأجزاء السيارات والأجهزة الإلكترونية والمعدات الخارجية والمكونات الصناعية المعرضة للبرد الشديد. توريد المصنع مباشرة: صياغة مواد قابلة للتخصيص لتلبية متطلبات الأداء والمعالجة المحددة.

  • Nylon 6 YH800 Grade
    PA6 YH800 راتنج نايلون 6 عالي الأداء من الدرجة البكر

    نايلون PA6 عالي الجودة من الدرجة العذراء: راتينج بولي أميد 6 (PA6) عالي الجودة وغير معدل مع تركيبة YH800، مما يضمن أداءً ثابتًا ومتانة استثنائية. التطبيقات الرئيسية: مثالي لأجزاء السيارات والأجهزة الإلكترونية والأدوات الكهربائية والمكونات الصناعية. توريد المصنع مباشرة: قابلة للتخصيص لتلبية متطلبات المعالجة والأداء المحددة.

عن Bocheng
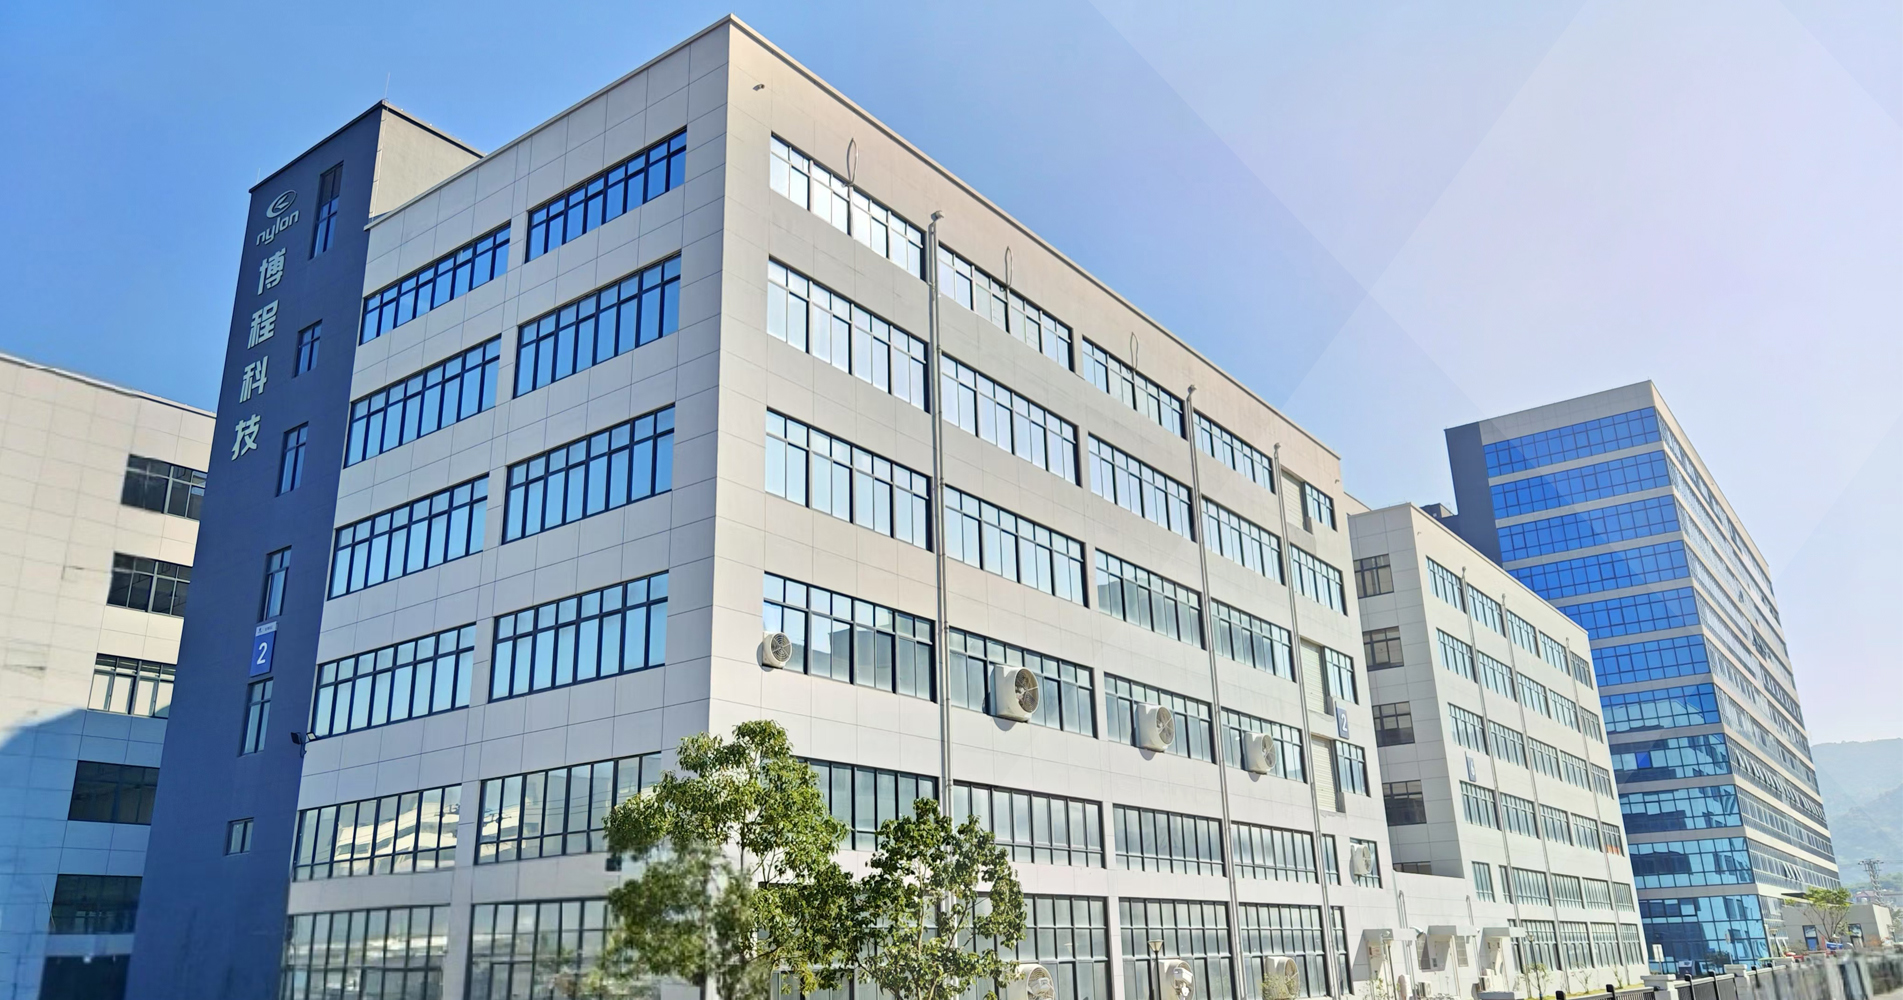
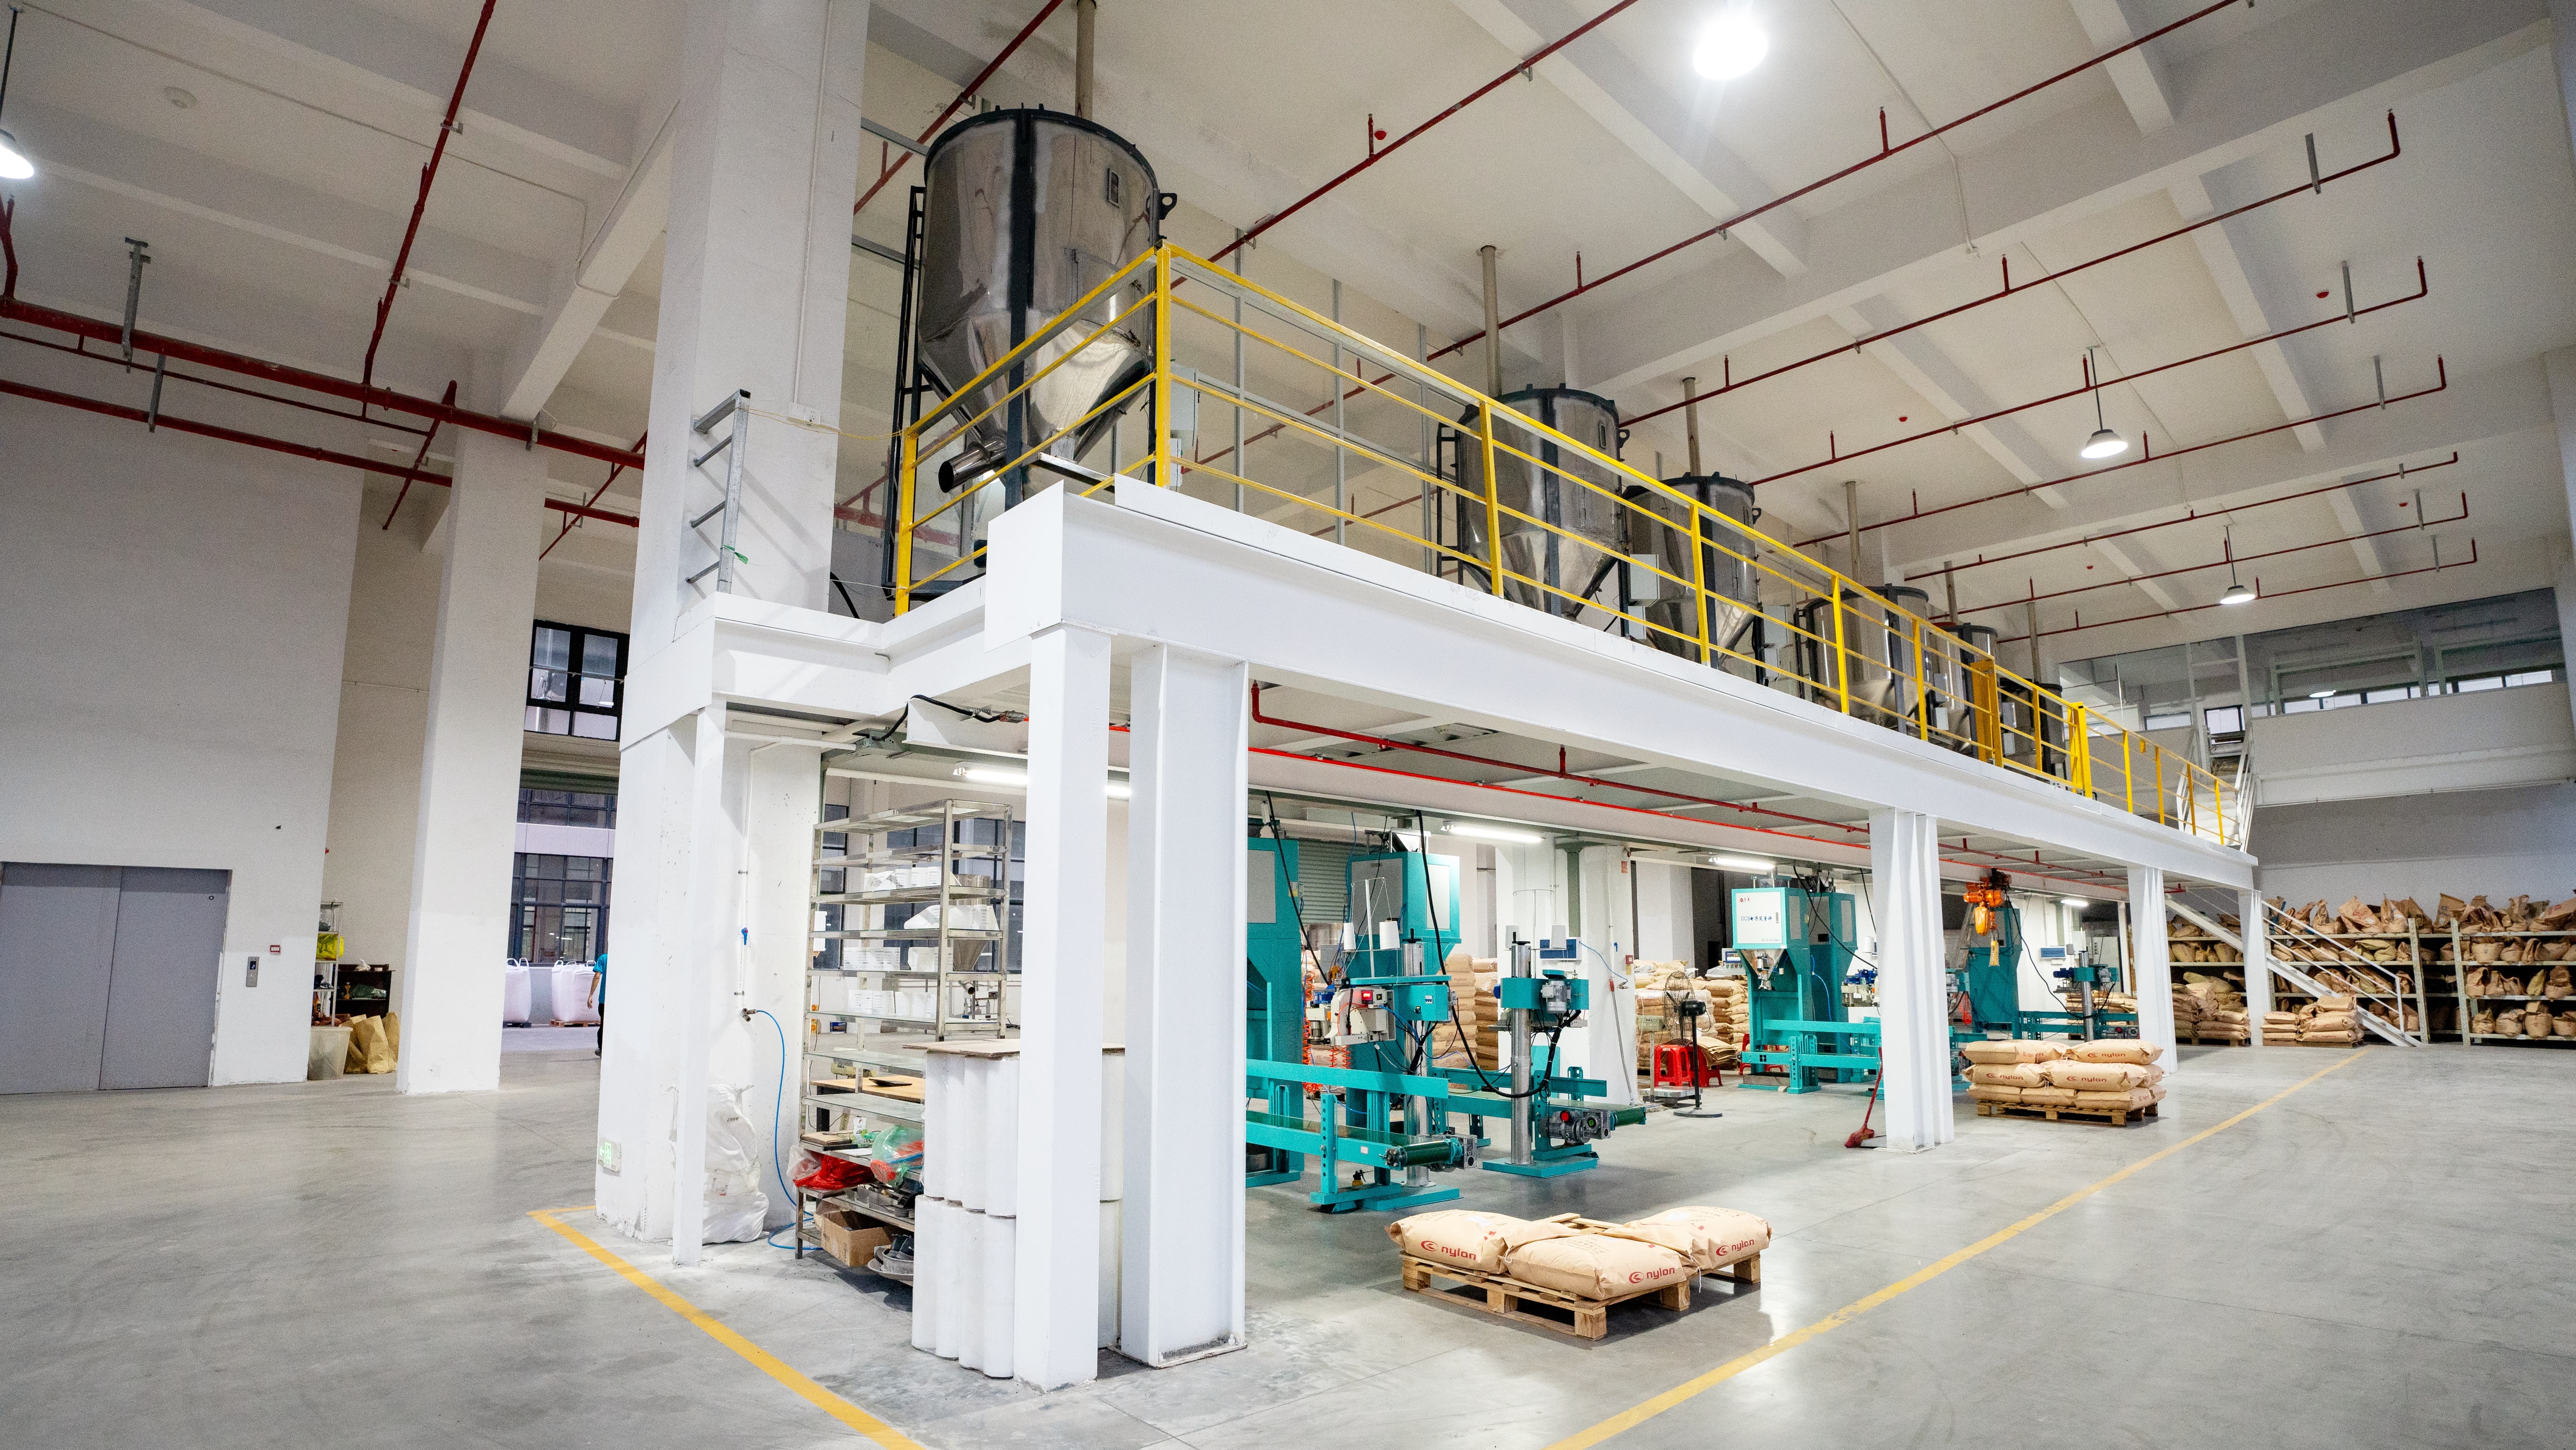
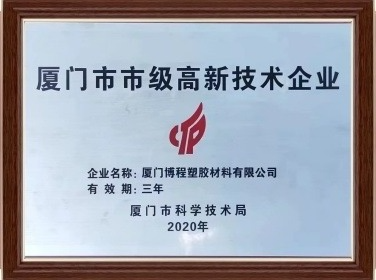
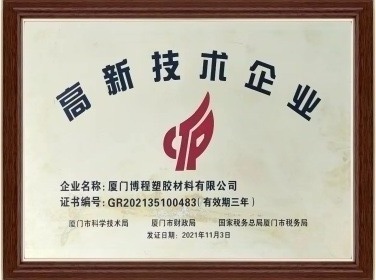
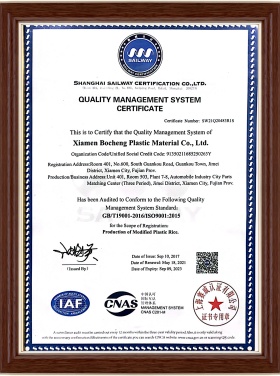
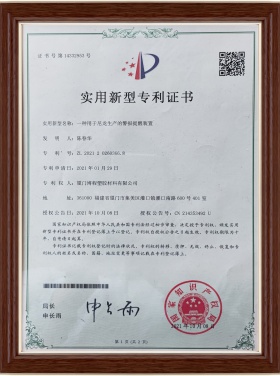
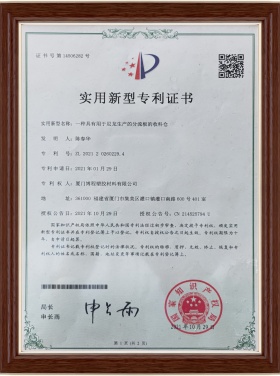
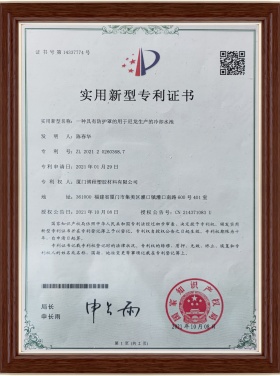
شركة Xiamen Bocheng Plastic Materials Co., Ltd. هي شركة رائدة في مجال الإنتاج الحديث، تأسست عام 2009، وتقع في المنطقة الاقتصادية الخاصة بشيامن، الصين. وبصفتنا شركة ملتزمة بالابتكار والتميز التكنولوجي، فإننا ندمج البحث والتطوير والإنتاج والمبيعات في مجال المواد البلاستيكية عالية الأداء. وعلى مر السنين، رسّخنا مكانتنا كشركة موثوقة في هذا المجال، وحصلنا على العديد من الأوسمة، بما في ذلك الاعتراف بنا كشركة بلدية للتكنولوجيا الفائقة في شيامن، ومؤسسة وطنية للتكنولوجيا الفائقة، ومؤسسة توحيد معايير متكاملة.
  • مقرر
    0

    وجد

  • التجارب
    0

    الدول المصدرة

الشركة المصنعة المهنية للنايلون

"توفير ضمانات قوية لتلبية احتياجات العملاء وجودة المنتج."

أحدث الأخبار والمدونة

ابقَ على اطلاع بأحدث الأخبار والرؤى من شركتنا. تُقدّم مدونتنا اتجاهات الصناعة، وابتكارات المنتجات، ووجهات نظر الخبراء حول مواد النايلون، وغيرها الكثير.
  • 12 November 2026
    ISO 9001 and IATF 16949 Quality Standards at a Certified PA66 70G30HSLR BK009 Factory

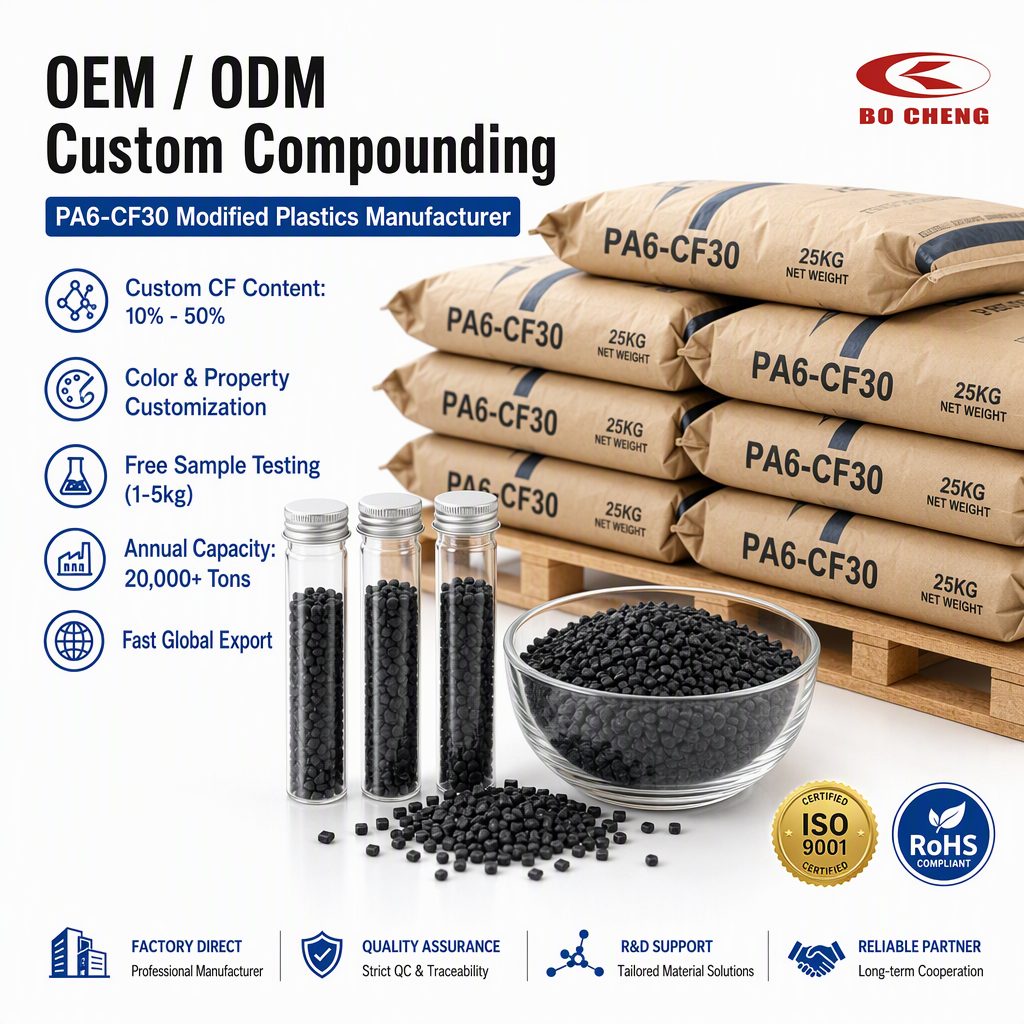
    Deconstructing Automotive-Grade Compliance: ISO 9001 and IATF 16949 Standards in Polyamide Compounding High-performance engineering plastics power critical components in modern automotive platforms and heavy industrial machinery. Modern original equipment manufacturers demand extreme mechanical strength, structural integrity, thermal stability, and long-term chemical resistance. Polyamide 66 reinforced with 30% glass fiber represents a primary workhorse compound for high-stress structural parts. However, achieving superior raw material performance on a laboratory scale differs significantly from delivering uniform quality across thousand-ton commercial shipments. Automotive supply chains require rigorous adherence to international quality management frameworks to guarantee zero-defect manufacturing. Sourcing engineering resins from a verified Certified PA66 70G30HSLR BK009 Factory gives tier-1 molders structural guarantees for critical under-the-hood components and heavy-duty mechanical assemblies. Standard ISO 9001 certification provides a foundation for systematic quality management, operational governance, and organizational consistency. However, the automotive sector demands the specialized IATF 16949 quality framework to address extreme field conditions. This stringent standard integrates Advanced Product Quality Planning and the Production Part Approval Process directly into daily compounding workflows. These engineering protocols emphasize defect prevention, continuous risk reduction, comprehensive failure mode identification, and total variation elimination across high-volume production runs. Consequently, certified compounding facilities maintain detailed control metrics across raw resin selection, fiber surface sizing, heat stabilizer loading, and twin-screw extrusion parameters.   The Five-Stage Quality Protocol: Mapping Standards into Everyday Manufacturing Translating high-level quality certifications into consistent physical properties requires an integrated testing protocol across every compounding step. Quality control begins during the raw material incoming inspection stage. Quality engineers test virgin PA66 base resin for relative viscosity, initial moisture content, and molecular weight distribution. Simultaneously, technical teams audit glass fiber strand length, sizing compatibility, and heat stabilizer purity prior to compounding. Controlling raw material inputs prevents batch-to-batch variations before processing ever begins. The second phase governs in-process quality control during twin-screw melt compounding. Extrusion monitoring systems track barrel temperature profiles, screw speed, torque, and vacuum degassing pressure in real time. Technicians verify the precise 30% glass fiber loading through burn-off ash testing at regular intervals. Furthermore, automated sampling checks matrix dispersion uniformity, anti-oxidant distribution, and heat stabilizer dispersion throughout continuous production runs. Stage three focuses on particle morphology and micro-milling consistency during pellet handling and transformation. Controlling granule size distribution, bulk density, and surface dust levels ensures uniform feeding behavior and consistent melting rates inside customer injection molding machines. Stage four applies advanced analytical characterization through differential scanning calorimetry and melt rheology testing. Thermal analysis determines melting point behavior, crystallization temperature, glass transition points, and enthalpy curves. Evaluating these thermodynamic markers eliminates thermal hysteresis and prevents molecular chain degradation during high-temperature compounding. The final stage completes outgoing quality verification through comprehensive Certificate of Analysis documentation. Quality teams pull random samples from each finished lot to perform standardized mechanical testing. Technicians measure tensile strength at yield, flexural modulus, Izod notched impact resistance, and heat deflection temperature under standardized environmental conditions. Outgoing shipments must meet exact specification thresholds before receiving final quality clearance for release. Traceability Architecture: Full-Lifecycle Genealogies from Granule to End Application A core pillar of IATF 16949 compliance involves establishing complete product traceability across the entire manufacturing lifecycle. Every production batch receives a unique digital identifier that links finished pellets back to original raw material lots, specific production operators, and machine run numbers. Automated warehouse management systems record raw material origin, continuous sensor logs, feeder calibration data, and final laboratory test results within a centralized database. This detailed data trail allows engineers to isolate process variables and conduct rapid root-cause diagnostics if field anomalies occur during molding operations. Systematic quality control becomes especially critical during the scale-up transition from pilot samples to full commercial production runs. Technical teams analyze process variations to bridge performance gaps during the transition from sample to mass production: engineering root cause analysis of nylon material performance improvement. Identifying subtle thermal shifts, filler degradation, or fiber orientation issues during early production prevents costly mold modifications and scrap generation later. Documented process stability prevents unexpected mold shrinkage variation, warpage, or mechanical drop-offs during high-speed injection molding. Enterprise Quality Infrastructure & Certification Verification Executing rigorous automotive quality standards requires advanced processing infrastructure, automated control systems, and certified laboratory testing facilities. Industrial compounder BOCHENG (Xiamen Bocheng Plastic Materials Co., Ltd) maintains specialized production lines dedicated to high-strength polyamide compounding. The facility operates under certified quality management systems, including ISO 9001:2015 certificate CN19/31332 and IATF 16949:2016 certificate 0380315, issued by international accredited registrar bodies. These official credentials confirm that manufacturing operations adhere strictly to global quality control standards. With an annual engineering plastic production capacity exceeding 15,000 tons, BOCHENG delivers consistent material supplies for demanding global applications. The enterprise manufactures specialized formulations, including heat-stabilized, hydrolysis-resistant, glycol-resistant, and black pigmented grades like PA66 70G30HSLR BK009. These materials supply major automotive suppliers for engine covers, intake manifolds, cooling system modules, thermostat housings, and structural electrical connectors. Partnering with a Certified Polymer Engineering Pioneer Sourcing engineering plastics from a certified manufacturer provides significant competitive advantages for tier-1 suppliers and industrial molders. In-house compounding expertise allows technical teams to adjust glass fiber loading, thermal stabilizers, flame retardants, and color matrices to meet custom customer specifications. Direct collaboration with experienced polymer engineers streamlines material qualification cycles, minimizes tool tuning, and shortens time-to-market for complex engineering projects. Transparent procurement practices give international clients direct access to technical support and complete quality documentation. Enterprise buyers and quality auditors can verify official accreditation records, review complete product specifications, examine lot-specific inspection reports, and request validation samples for independent testing. Partnering with a certified compounding specialist establishes reliable material supply chains, protects brand equity, and ensures long-term part reliability in demanding end-use applications. Discover verified polyamide manufacturing capabilities and quality documentation at: https://www.pa6-pa66.com/.
  • 12 November 2026
    Ensuring SGS RoHS and REACH Compliance: Quality Audit Criteria for a Certified PA612 CF40 Supplier

    Regulatory Risk Mitigation: Converting Environmental Compliance into Procurement Security Global environmental regulations shape material procurement strategies across automotive, electronics, and industrial manufacturing sectors. Strict regulatory frameworks, including the European Union RoHS directive, REACH SVHC candidate lists, and TSCA guidelines, restrict hazardous chemicals in engineering thermoplastics. Non-compliant components expose international manufacturers to customs impoundments, heavy regulatory fines, product recalls, and severe brand equity damage. Industrial buyers must evaluate environmental compliance alongside mechanical strength, thermal resistance, and dimensional stability. Sourcing high-performance carbon-fiber-reinforced polyamides from a qualified Certified PA612 CF40 Supplier mitigates regulatory liability while guaranteeing material integrity for mission-critical structural assemblies. Environmental risk management requires moving beyond superficial compliance claims. Supply chain auditors must establish proactive screening frameworks to verify chemical purity across all raw material inputs. Specialized engineering polymers, such as polyamide 612 reinforced with 30% or 40% carbon fiber, utilize complex chemical additive packages. Coupling agents, sizing treatments, anti-oxidants, and color masterbatches can inadvertently introduce restricted substances into the final plastic compound. Consequently, tier-1 suppliers implement rigorous supplier audit protocols to ensure uncompromised chemical purity from raw monomer synthesis to final granule packaging.   The Procurement Audit Checklist: Four Pillars of Environmental Assurance Procurement teams rely on a structured four-pillar audit protocol to evaluate material suppliers effectively. The first pillar focuses on hazardous substance restriction verification. Auditors verify that engineering resins comply fully with RoHS 2.0 requirements, restricting ten core hazardous substances. Testing covers heavy metals, polybrominated biphenyls, polybrominated diphenyl ethers, and four specific phthalate plasticizers. Furthermore, evaluation routines verify that chemical concentrations remain well below the 0.1% weight threshold established by international environmental authorities. The second pillar requires full material disclosure through supply chain chemical declarations. Certified compounding facilities maintain transparent chemical inventories for base resins, carbon fiber sizing agents, internal lubricants, and functional additives. Establishing complete material traceability ensures that no undocumented additives enter twin-screw extrusion lines during continuous production. Pillar three centers on third-party analytical verification through accredited testing protocols. Leading industrial compounders partner with internationally recognized laboratories, such as SGS or TUV, to conduct rigorous chemical testing. Laboratory technicians utilize advanced analytical methods, including gas chromatography-mass spectrometry and inductively coupled plasma optical emission spectrometry, following IEC 62321 international testing standards. The final pillar establishes mandatory renewal rhythms and batch-level audit protocols. Annual laboratory re-certifications verify long-term formulation compliance. Simultaneously, incoming raw material batches undergo lot-by-lot X-ray fluorescence screening prior to processing. Combining annual full-scan third-party testing with continuous internal screening prevents hazardous cross-contamination across production runs. Advanced Polymer Selection Matrices: Comparing Polyamide Variants Understanding environmental compliance becomes even more critical when evaluating broader engineering plastic families. Technical insights from a PA6 GF30 vs PA66 GF30 material selection matrix from a high quality 30 glass fiber reinforced nylon 6 supplier highlight how material selection impacts both physical performance and regulatory stability. Polyamide 6 reinforced with 30% glass fiber provides excellent surface aesthetics, easier processing characteristics, and cost-effectiveness for general industrial housings. In contrast, polyamide 66 reinforced with 30% glass fiber delivers superior thermal endurance, higher tensile modulus, and greater creep resistance under elevated temperatures, making it the preferred choice for heavy-duty automotive engine compartments. However, standard short-chain polyamides absorb significant ambient moisture, which affects dimensional stability and mechanical stiffness over time. Long-chain polyamides, such as polyamide 612 reinforced with carbon fiber, offer a superior technical solution. Carbon-fiber-reinforced PA612 grades exhibit dramatically reduced moisture absorption, exceptional dimensional precision, and outstanding stiffness-to-weight ratios. These properties make PA612 CF30 and CF40 compounds ideal for precision aerospace brackets, robotics components, and high-speed mechanical drives where environmental exposure is severe. Electrical Housing Safety and Halogen-Free Flame Retardancy Safety standards in electrical and electronic applications require specialized compounding solutions that balance mechanical strength with rigorous flame retardancy. Insights from an electrical housing safety insights from a high quality PA66 GF30 FR V0 supplier emphasize the critical importance of halogen-free flame retardant systems. Traditional electrical housings relied on halogenated compounds containing bromine or chlorine, which released toxic corrosive gases during combustion and faced increasing regulatory pressure under global environmental directives. Modern engineering compounding replaces halogenated additives with eco-friendly phosphorus-nitrogen flame retardant formulations. These advanced systems enable reinforced polyamides to achieve UL94 V-0 flammability ratings at minimal wall thicknesses while maintaining high Comparative Tracking Index (CTI) performance and excellent Glow Wire Ignition Temperature (GWIT) ratings. Integrating halogen-free flame retardants ensures that electrical enclosures meet strict international safety certifications without violating RoHS or REACH restricted substance limits.   BOCHENG’s Environmental Quality Assurance Framework Delivering eco-compliant engineering thermoplastics requires advanced compounding technology and rigorous quality management systems. Industrial resin manufacturer BOCHENG (Xiamen Bocheng Plastic Materials Co., Ltd) operates modern production facilities backed by ISO 9001 and IATF 16949 quality management certifications. With an annual production capacity exceeding 15,000 tons, BOCHENG provides consistent material supplies for demanding global applications. Technical teams enforce strict quality controls across every compounding stage to guarantee full chemical compliance. BOCHENG maintains up-to-date SGS test reports verifying non-detectable levels across RoHS restricted substances and REACH SVHC candidate lists. These traceable compliance documents cover premium carbon-fiber-reinforced grades, including PA612 CF30 and PA612 CF40 granules, alongside flame-retardant electrical grades. Enterprise procurement officers can review complete technical documentation, verify third-party test reports, and request validation sample batches for independent laboratory screening. Direct manufacturer partnership ensures long-term regulatory compliance, robust material availability, and reliable part performance in critical industrial applications. Explore verified eco-compliant engineering thermoplastics at: https://www.pa6-pa66.com/.
  • 08

    2026-05

    من العينة إلى الإنتاج الضخم: تحليل الأسباب الجذرية الهندسية لتحسين أداء مادة النايلون 2

    يتضمن مثال عملي غلاف موصل سيارة مصنوع من PA66 GF30أثناء عملية التكلس، أدى خفض درجة حرارة القالب من 90 درجة مئوية إلى 70 درجة مئوية إلى تحسين زمن الدورة، ولكنه قلل من مقاومة الصدمات بنسبة 15% تقريبًا، مما أدى إلى الفشل. وقد حلّت استعادة درجة حرارة القالب الأصلية المشكلة. مع تسليط الضوء على اعتماد الأداء على ظروف العملية.ترتبط حركية تبلور البولي أميد ارتباطاً مباشراً بمعدل التبريد والخواص الميكانيكية. فالتبريد الأسرع يزيد من الصلابة ولكنه يقلل من المتانة. يُعد الحفاظ على هذا التوازن أمراً ضرورياً ولكنه غالباً ما يتعرض للخطر في الإنتاج عالي الإنتاجية.تؤكد البيانات هذه الاتجاهات: يمكن أن تختلف قوة التأثير على طول 20% مع تقلبات الرطوبة، وتحولات معامل الانحناء بواسطة 10-15% مع تغيرات درجة حرارة القالب. هذه الاختلافات كبيرة بما يكفي للتأثير على موثوقية المنتج.في نهاية المطاف، لا يتعلق تحسين الأداء باختيار مادة أفضل، بل بالتحكم في نظام المعالجة. ينبغي على المهندسين إعطاء الأولوية لمعايير التجفيف، ونطاقات درجة حرارة القالب، وحدود القص لضمان الاتساق. 

    اقرأ المزيد
  • 08

    2026-05

    من العينة إلى الإنتاج الضخم: تحليل الأسباب الجذرية الهندسية لتحسين أداء مادة النايلون 1

    من التحقق من صحة النموذج الأولي إلى الإنتاج الضخم، تتغير الأداء في بولي أميد كثيراً ما يُساء فهم هذه الظاهرة على أنها عدم تجانس في المادة، بينما هي في الواقع ناتجة عن تغيرات في ظروف التصنيع. في بيئات المختبرات المُحكمة، تُنتج العينات المقولبة بالحقن في ظل ظروف تجفيف مستقرة، وقص منخفض، ودرجات حرارة مثالية للقالب. مع ذلك، عند الانتقال إلى الإنتاج على نطاق واسع، تُغير الاختلافات في محتوى الرطوبة، وزمن الدورة، وتاريخ القص بشكل كبير من سلوك المادة.البولياميد شديد الحساسية للرطوبة. فقد يؤدي تغير طفيف في نسبة الرطوبة، يتراوح بين 0.08% و0.2%، إلى انخفاض ملحوظ في مقاومة الصدمات وزيادة في عيوب السطح. وفي الإنتاج الضخم، تُحدث عمليات مناولة المواد والرطوبة المحيطة تقلبات في الرطوبة حتى قبل دخول المادة إلى آلة التشكيل.تُعدّ تحولات نافذة المعالجة عاملاً رئيسياً آخر. فزيادة سرعات الحقن وتقصير الدورات يزيدان من معدلات القص، مما يُحسّن من توجيه الجزيئات وتباينها. ويتضح هذا جلياً في PA66 المقوى بالألياف الزجاجية، حيث يؤثر محاذاة الألياف على الانحناء والاستقرار الأبعاد.تزيد اختلافات الأدوات من تعقيد عملية التوسيع. تُحدث القوالب متعددة التجاويف اختلالاً في التدفق وتدرجات حرارية، مما يؤثر على سلوك التبلور وتناسق الانكماش. غالباً ما تُعزى هذه المشكلات خطأً إلى اختلاف المواد بدلاً من انحراف العملية.

    اقرأ المزيد
  • 23

    2026-04

    نموذج مقارن لتكلفة دورة حياة PA6 و PA66 والنايلون المعاد تدويره 2

    مع ذلك، تُؤدي هذه الميزة الهيكلية إلى بعض التنازلات. يتطلب البولي أميد 66 درجات حرارة معالجة أعلى، ويستهلك عادةً طاقة أكبر أثناء عملية التشكيل بالحقن. في بيئات التصنيع واسعة النطاق، تؤثر هذه الاختلافات على استهلاك الطاقة في الآلات، ووقت التبريد، ومدة دورة القالب.تصبح المقارنة أكثر تعقيدًا عندما يتم إدخال النايلون المعاد تدويره في عملية اختيار المواد. يُستخلص النايلون المعاد تدويره عادةً من مخلفات ما بعد الصناعة أو نفايات ما بعد الاستهلاك. بعد التنظيف وإعادة التركيب والتثبيت، يمكن إعادة إدخال المادة في دورة الإنتاج كمادة خام للبلاستيك الهندسي.من أهم مزايا النايلون المعاد تدويره انخفاض بصمته الكربونية بشكل ملحوظ مقارنةً بإنتاج البوليمر الخام. إضافةً إلى ذلك، فإن سعر المواد المعاد تدويرها يكون أحيانًا أقل تأثرًا بتقلبات أسواق المواد الخام البتروكيماوية. ومع ذلك، لا تزال المخاوف بشأن استقرار الخصائص وتناسق الدفعات تتطلب التحقق الهندسي الدقيق.تُظهر تجارب العديد من مشاريع التصنيع أن سعر المواد الخام وحده نادرًا ما يُحدد النتيجة الاقتصادية النهائية. على سبيل المثال، في مشروع مكونات هيكلية للأجهزة المنزلية، بدا البولي أميد 6 (PA6) في البداية المادة الأكثر فعالية من حيث التكلفة نظرًا لانخفاض سعره مقارنةً بـ PA66. ومع ذلك، كشفت اختبارات التقادم طويلة المدى أن المكون فقد تدريجياً استقراره الأبعاد عند تعرضه لدرجات حرارة تشغيل مستمرة تبلغ حوالي 90 درجة مئوية.وللتعويض عن هذا التأثير، اضطر المهندسون إلى زيادة سُمك جدار تصميم المكون. وقد أدى هذا التعديل إلى زيادة إجمالي استهلاك المواد، وتطلب إجراء تعديلات على هيكل قالب الحقن. ونتيجة لذلك، تراجعت الميزة السعرية الأولية لـ PA6 انخفض بشكل ملحوظ.لوحظ وضع مماثل في بعض مكونات المركبات الكهربائية. فقد اختارت بعض برامج التصميم الأولية مواد النايلون منخفضة التكلفة لتقليل سعر المكونات المبدئي. إلا أنه خلال اختبارات التدوير الحراري طويلة الأمد، ظهرت تشققات ناتجة عن الإجهاد أو تشوهات في الأبعاد في عدة أجزاء. وقد أدى استبدال المادة بمادة البولي أميد المقاومة للحرارة العالية إلى زيادة سعر المادة، ولكنه قلل من خطر تعطل المكونات أثناء تشغيل المركبة.توضح هذه الأمثلة سبب تزايد أهمية التفكير في دورة حياة المنتج في اختيار المواد الهندسية. فبدلاً من التركيز فقط على تكلفة المواد الخام، يُقيّم المهندسون التأثير المُجتمع لعوامل متعددة عبر دورة حياة المنتج بأكملها.يتضمن نموذج تكلفة دورة الحياة المبسط لمواد النايلون عادةً تكلفة شراء المواد الخام، واستهلاك طاقة المعالجة، وكفاءة الإنتاج، وعمر خدمة المنتج، وقيمة إعادة التدوير المحتملة في نهاية الاستخدام. من خلال تحليل هذه المعايير معًا، يصبح من الأسهل فهم الأداء الاقتصادي الحقيقي لأنظمة المواد المختلفة.على سبيل المثال، في التطبيقات الإنشائية ذات درجات الحرارة العالية، قد يبدو البولي أميد 66 أغلى ثمناً على مستوى المواد الخام. مع ذلك، إذا حسّنت هذه المادة بشكل ملحوظ من متانة المنتج وقللت من مخاطر الفشل، فقد تصبح التكلفة الإجمالية لدورة حياة المنتج أقل من تكلفة البولي أميد 66.في المقابل، غالباً ما يُظهر البولي أميد 6 (PA6) مزايا واضحة في المكونات ذات الجدران الرقيقة والأشكال الهندسية المعقدة. تسمح سيولته الفائقة بضغط حقن أقل وأوقات تعبئة أقصر، مما يُحسّن الإنتاجية في بيئات الإنتاج الضخم.يُضفي النايلون المُعاد تدويره بُعدًا جديدًا على تقييم تكلفة دورة الحياة. تكمن قيمته الأساسية في خفض انبعاثات الكربون والامتثال للوائح التنظيمية، وليس في الفوائد الاقتصادية البحتة. ومع تزايد شيوع الإفصاح عن البصمة الكربونية في سلاسل التوريد الأوروبية، بدأ مصنّعو السيارات في طلب توثيق محتوى المواد المُعاد تدويرها في البلاستيك الهندسي.في ظل هذه الظروف، لا يُعد النايلون المعاد تدويره مجرد اعتبار للتكلفة فحسب، بل هو أيضاً جزء من استراتيجية استدامة أوسع نطاقاً ضمن سلسلة التوريد.بالنظر إلى المستقبل، سيتجه اختيار المواد الهندسية تدريجياً من مجرد مقارنة الأسعار إلى تقييم شامل لدورة حياة المنتج. يجب على المهندسين الموازنة بين الأداء الميكانيكي، وكفاءة التصنيع، والموثوقية على المدى الطويل، والأثر البيئي عند الاختيار بين مواد PA6 وPA66 والنايلون المعاد تدويره.موردي المواد القادرين على توفير بيانات موثوقة عن دورة حياة المنتج، بما في ذلك اختبار المتانة وتحليل البصمة الكربونيةمن المرجح أن تكتسب مكانة أقوى في سلاسل توريد المواد الهندسية المستقبلية.

    اقرأ المزيد

ترك رسالة

ترك رسالة
إذا كنت مهتمًا بمنتجاتنا وتريد معرفة المزيد من التفاصيل، فيرجى ترك رسالة هنا، وسوف نقوم بالرد عليك في أقرب وقت ممكن.
يُقدِّم

بيت

منتجات

WhatsApp

اتصال